WINVERA / MODULAR DRILLING
Modular Drill Bodies & Replaceable Head Systems
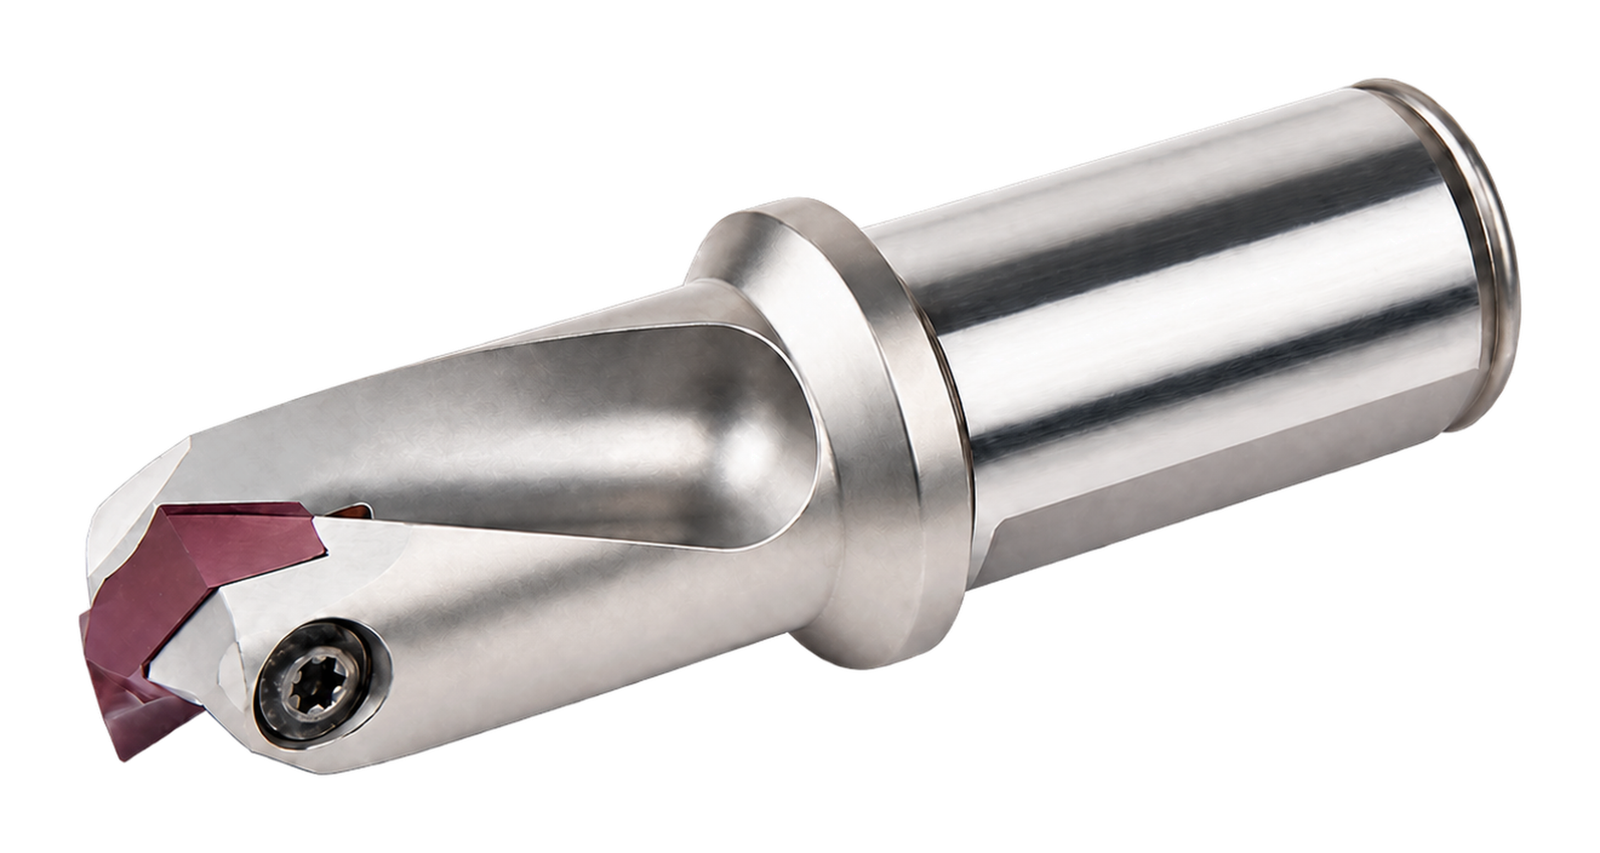
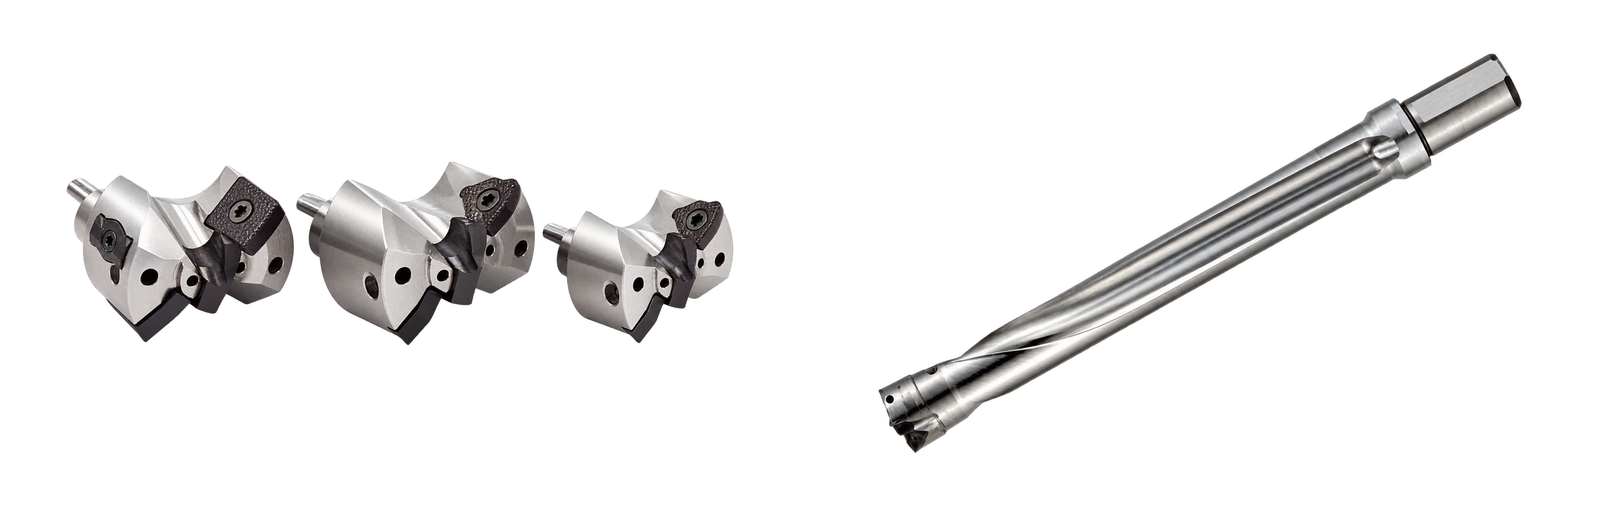
A modular drill (also called a replaceable-head drill, RHD modular drill, or crown drill) pairs a reusable steel drill body with a carbide cutting head or tip. You select the body for hole diameter and drilling depth (L/D), then match a head geometry and grade to the workpiece—without replacing the entire tool when the cutting edge wears. Winvera modular families (WVT, WVC, WVV, WVFI and WVFK) keep body and head interfaces within each family; diameters and depth groups are listed in the tables below.
How to choose a modular / crown drill
A short buyer guide: diameter and L/D first, then WVT / WVC / WVV / WVFI / WVFK — with when modular beats solid carbide. Read the selection guide →
01 / PRODUCT FAMILIES
Find your drilling system


02 / PRODUCT FINDER
Find your modular drilling tools
Product finder
03 / SELECTION
How to select a modular drill body and head
1. Diameter and depth first
Choose the shortest L/D that reaches the hole.
2. Pick family
WVFI/WVFK smaller (~Ø10–33); WVT broad geometries; WVC GG tip + R3–R10; WVV large (body IF + module IF must match).
3. Match cutting component within that family only
4. Material → geometry (and grade)
After you lock diameter, L/D and family, choose the carbide head geometry for the workpiece group, then confirm the grade on that head’s Application Data. The matrix below is the WVT starting map (ISO P / M / K / N / S). Exact diameter bands, coatings and cutting data stay on the linked head pages—do not treat this hub table as a cutting-data sheet.
| ISO group | Start geometry | Typical grades | Head pages |
|---|---|---|---|
| P — steel | PG first also GG, PL, E, PCM |
WV3015: P M K WV3010: P M K S (PG) |
PG · GG · PL · E · PCM |
| M — stainless | MG first also PG, PL, E, PCM |
MG: WV3015 M · WV3010 M | MG (+ PG/PL/E/PCM) |
| K — cast iron | GG or PG also PL, E, PCM |
GG: WV3015/WV3010 P K | GG · PG |
| N — non-ferrous | PCM | WV3015: P M K N S | PCM |
| S — heat-resistant / Ti | PCM or PG where S is listed |
PCM WV3015 includes S PG WV3010 includes S |
PCM · PG |
Geometry quick legend (WVT)
PG — general first pick · Ø12.50–54 · WV3015 (P M K), WV3010 (P M K S)
GG — lower force, P/K · Ø12.50–40 · WV3015/WV3010 (P K)
PL — guidance / less burr · P M K · Ø12.50–40
MG — stainless-first · Ø12.50–40 · WV3015/WV3010 (M)
E — flat / ~180° bottoms · P M K · Ø16–40
PCM — centering / pre-drill · widest incl. N,S · Ø12.50–40 · WV3015 (P M K N S)
Other families — do not paste the WVT table onto them
WVC — GG tip only with R3/R5/R7/R10 · see WVC GG tips
WVV — PG/PL tips + inserts/modules · body IF must match module IF · WVV series
WVFI / WVFK — confirm geometry on the WVFI/WVFK series page
Rule: material group → geometry → grade. Final combo from the head’s Application Data. Unclear alloys: RFQ with grade and hardness.
5. Confirm coolant, screws/keys, shank fit and runout
Coolant capability depends on the exact body and head pair—Winvera does not publish one universal bar or MPa value for every modular assembly. Before the first cut, work this checklist against the body and head Application Data and your machine:
- Confirm the body is specified for through-tool coolant if the process needs internal coolant.
- Check seals, fittings and holder passages so the coolant path is continuous to the head.
- For longer L/D groups (about 8×D–12×D), prefer reliable internal coolant and chip evacuation; do not increase overhang without confirmed coolant delivery.
- Use only the screws / keys supplied for that documented body–head pair.
- Verify shank / holder fit and measure runout before cutting.
- Never mix heads across WVT, WVC, WVV, WVFI or WVFK. On WVV, body IF and module IF must match.
Exact vc / f and coolant pressure limits: use Application Data on the selected SKU pages—do not invent numbers on this hub.
04 / QUICK ANSWERS
Modular drilling questions
APPLICATION SUPPORT
Specify the hole. Select the system.
Send the hole diameter, depth, workpiece grade, hardness and machine connection with your enquiry.