Home / Threading Tools / WTP Straight Flute
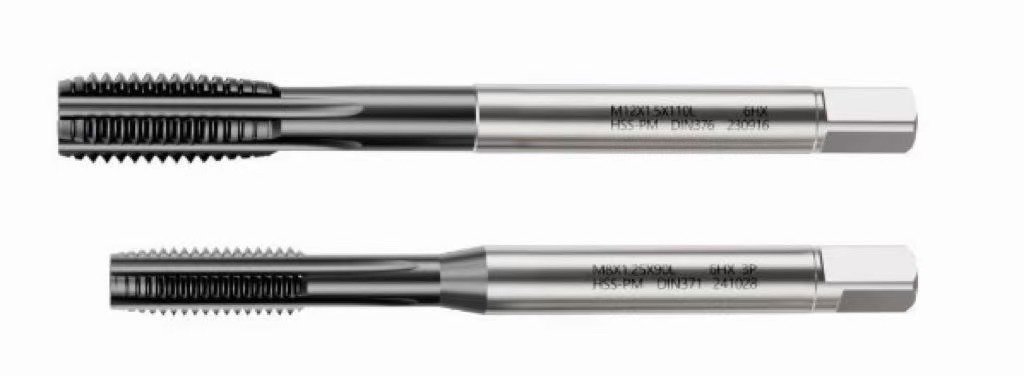
THREADING / WTP Straight Flute
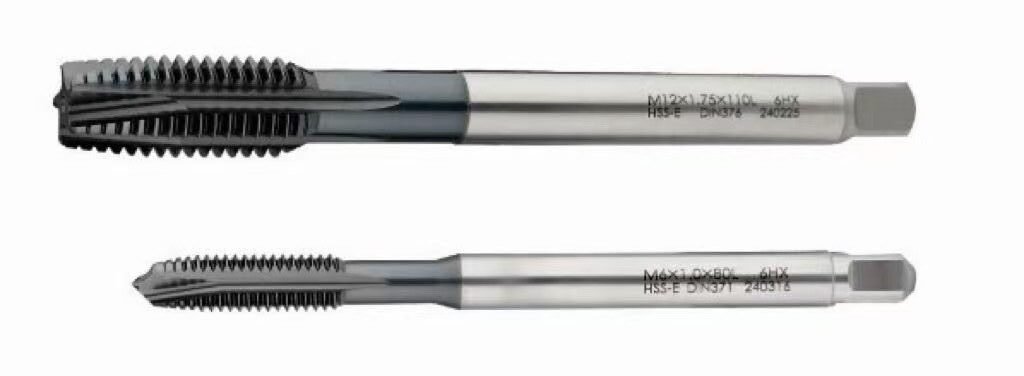
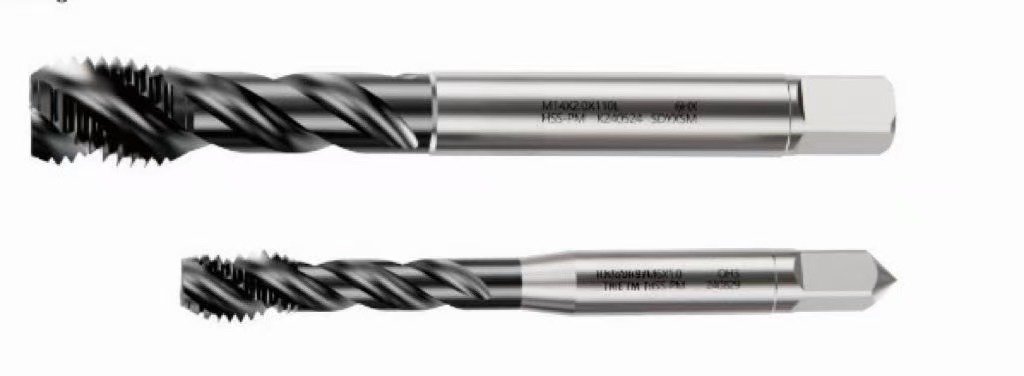
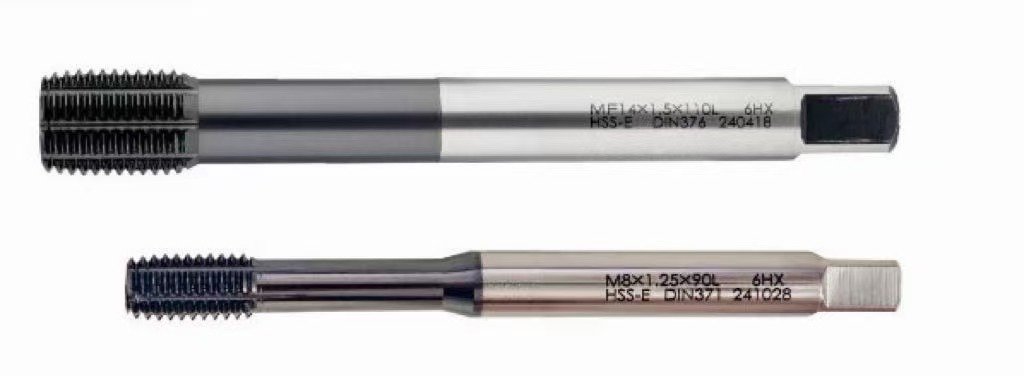
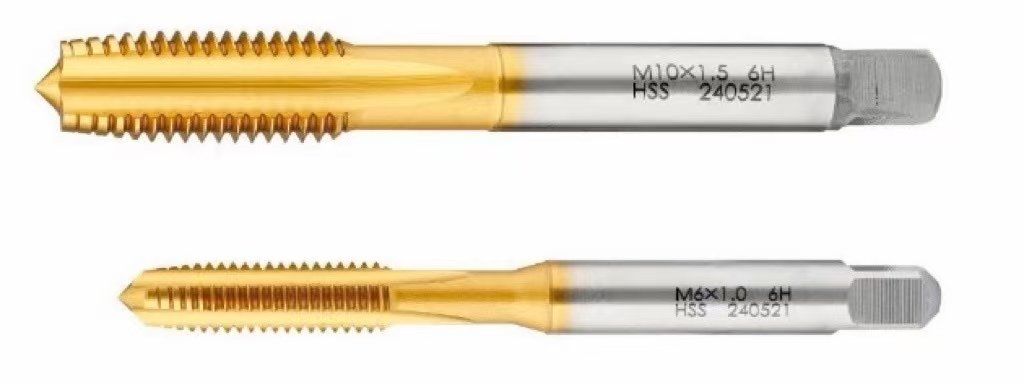
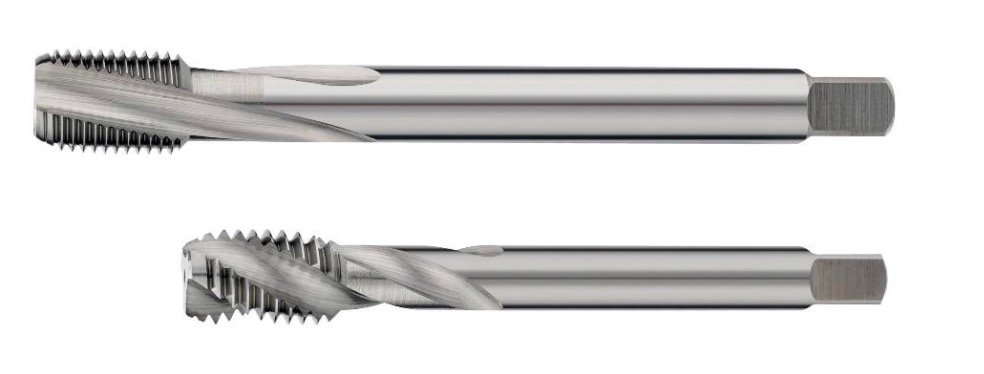
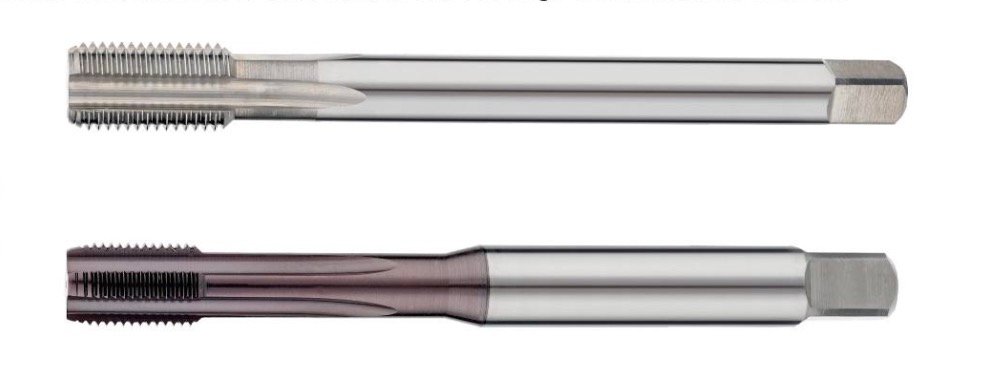
DIN Straight Flute Taps
Powder metallurgy HSS straight flute taps for cast iron and other short-chipping materials.
M3–M16 · DIN 371 / 376 / 374
Model Specifications
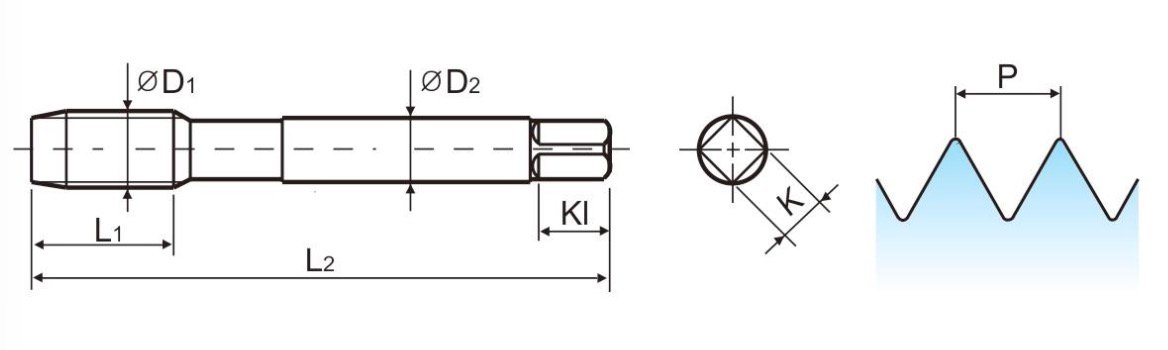
Dimensions are in millimetres. Select the thread diameter, pitch and complete EDP order code.
| Thread D1 | Pitch P (mm) | EDP order code | Tolerance | Overall L2 (mm) | Thread L1 (mm) | Shank D2 (mm) | Square K (mm) | Square length Kl (mm) | Flutes |
|---|---|---|---|---|---|---|---|---|---|
| M3 | 0.5 | SP7099206 | 6HX | 56 | 9 | 3.5 | 2.7 | 6 | 3 |
| M4 | 0.7 | SP7099246 | 6HX | 63 | 13 | 4.5 | 3.4 | 6 | 3 |
| M5 | 0.8 | SP7099286 | 6HX | 70 | 14 | 6 | 4.9 | 8 | 3 |
| M6 | 1 | SP7099316 | 6HX | 80 | 15 | 6 | 4.9 | 8 | 4 |
| M8 | 1 | SP7099376 | 6HX | 90 | 18 | 8 | 6.2 | 9 | 4 |
| M8 | 1.25 | SP7099366 | 6HX | 90 | 18 | 8 | 6.2 | 9 | 4 |
| M10 | 1 | SP7099446 | 6HX | 100 | 20 | 10 | 8 | 11 | 4 |
| M10 | 1.25 | SP7099436 | 6HX | 100 | 20 | 10 | 8 | 11 | 4 |
| M10 | 1.5 | SP7099426 | 6HX | 100 | 20 | 10 | 8 | 11 | 4 |
| M12 | 1.25 | SP7099526 | 6HX | 110 | 24 | 9 | 7 | 10 | 5 |
| M12 | 1.5 | SP7099516 | 6HX | 110 | 24 | 9 | 7 | 10 | 5 |
| M12 | 1.75 | SP7099506 | 6HX | 110 | 24 | 9 | 7 | 10 | 5 |
| M14 | 1.5 | SP7099556 | 6HX | 110 | 26 | 11 | 9 | 12 | 5 |
| M14 | 2 | SP7099546 | 6HX | 110 | 26 | 11 | 9 | 12 | 5 |
| M16 | 1.5 | SP7099616 | 6HX | 110 | 27 | 12 | 9 | 12 | 5 |
| M16 | 2 | SP7099606 | 6HX | 110 | 27 | 12 | 9 | 12 | 5 |
Workpiece Materials
PSteel KCast Iron NNon-ferrous Metals SHeat-resistant Superalloys and Titanium Alloys
Features & Parameters
DIN
Tool standard
371 / 376 / 374
HSS-PM
Tool material
Powder metallurgy HSS
6HX
Tap tolerance
Metric thread
2.5P / 5.0P
Chamfer lead
In thread pitches
60°
Thread angle
Metric profile
2.0 × D1
Tapping depth
Blind & through holes
Vap
Surface finish
Bright
Surface finish
TiN
Surface finish
Workpiece Suitability
| Material group | Workpiece material | Condition / grade | Suitability |
|---|---|---|---|
| PSteel | High-carbon steel | C ≥ 0.45% | Excellent |
| PSteel | Tool steel | SKD | Good |
| KCast Iron | Cast iron | FC | Excellent |
| KCast Iron | Ductile cast iron | FCD | Good |
| NNon-ferrous Metals | Cast aluminium alloys | AC / ADC | Good |
| SHeat-resistant Superalloys and Titanium Alloys | Titanium alloys | Good | |
| SHeat-resistant Superalloys and Titanium Alloys | Nickel alloys | Good |
Cutting speeds & coolant
General starting values for straight flute taps. Adjust to the workpiece, tap finish, hole dimensions and machining conditions.
| Material group | Workpiece | Condition / grade | Speed Vc (m/min) | Neat oil | Water-soluble | Semi-dry | Dry |
|---|---|---|---|---|---|---|---|
| PSteel | High-carbon steel | C ≥ 0.45% | 6–9 | ◎ | ○ | — | — |
| PSteel | Tool steel | SKD | 6–9 | ◎ | — | — | — |
| KCast Iron | Cast iron | FC | 10–15 | ◎ | ○ | ○ | ○ |
| KCast Iron | Ductile cast iron | FCD | 7–12 | ◎ | ○ | ○ | — |
| NNon-ferrous Metals | Cast aluminium alloys | AC / ADC | 10–15 | ◎ | ○ | — | — |
◎, ○ and △ indicate the coolant ratings. A dash indicates no listed recommendation. Cutting speed is in m/min; spindle speed n = 1000 × Vc / (π × D1), with D1 in mm.
| Symbol | Meaning | Unit |
|---|---|---|
| D1 | Nominal thread diameter | mm |
| P | Thread pitch | mm |
| L2 | Overall length | mm |
| L1 | Thread length | mm |
| D2 | Shank diameter | mm |
| K | Square drive width | mm |
| Kl | Square drive length | mm |
| EDP | Complete product order code | — |
DIN 371: metric coarse threads M2–M10. DIN 376: metric coarse threads M11–M30. DIN 374: metric fine threads. Available sizes for this series are listed above.
Include the EDP code, surface finish, quantity, workpiece material and hardness, thread depth and coolant method with your enquiry.
EXPLORE THE RANGE