Home / Threading Tools / WTP-NRT
THREADING / WTP-NRT
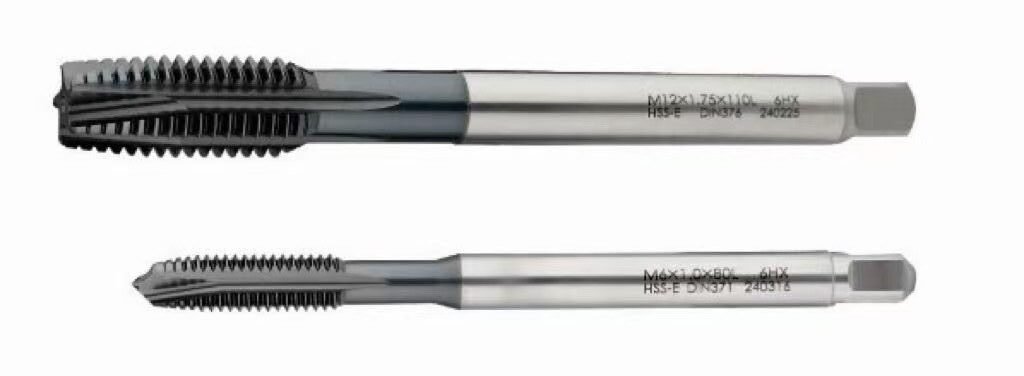
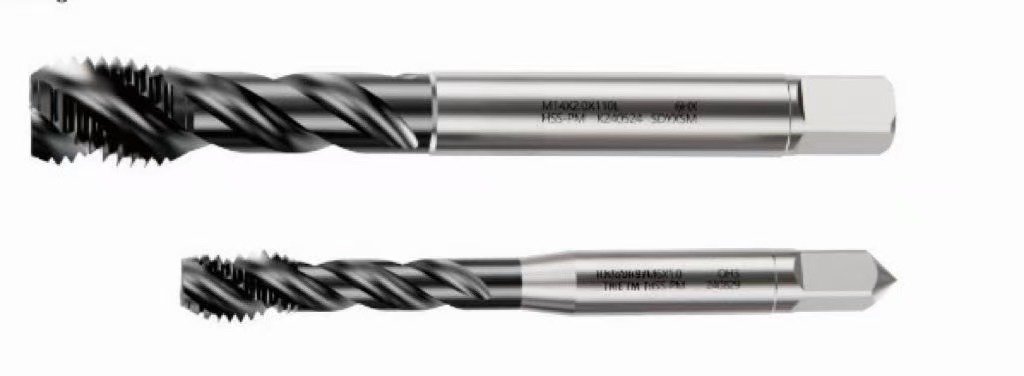
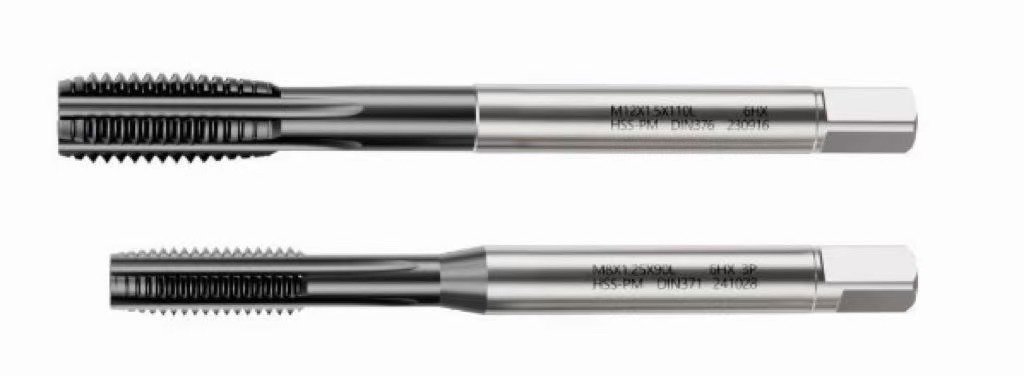
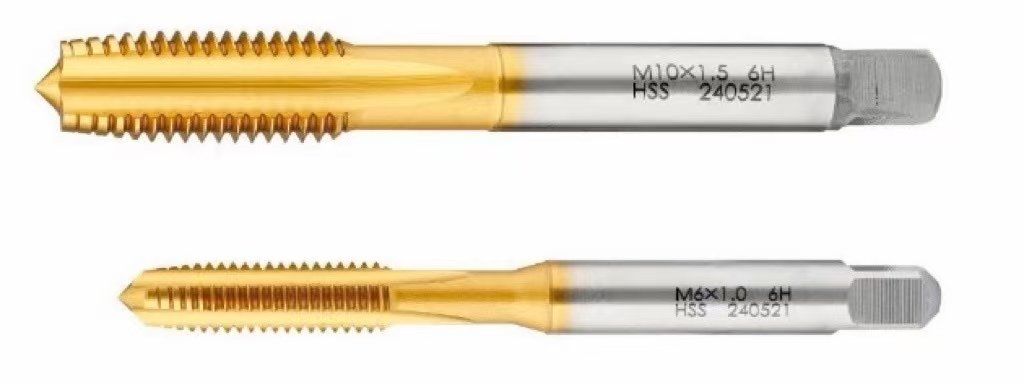
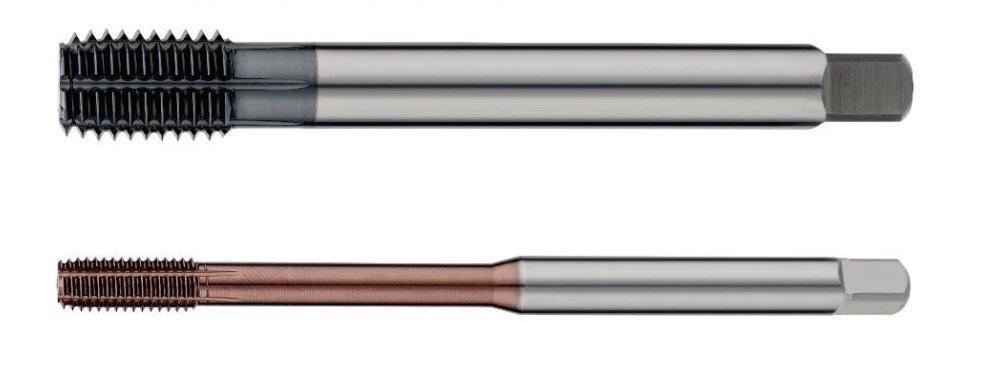
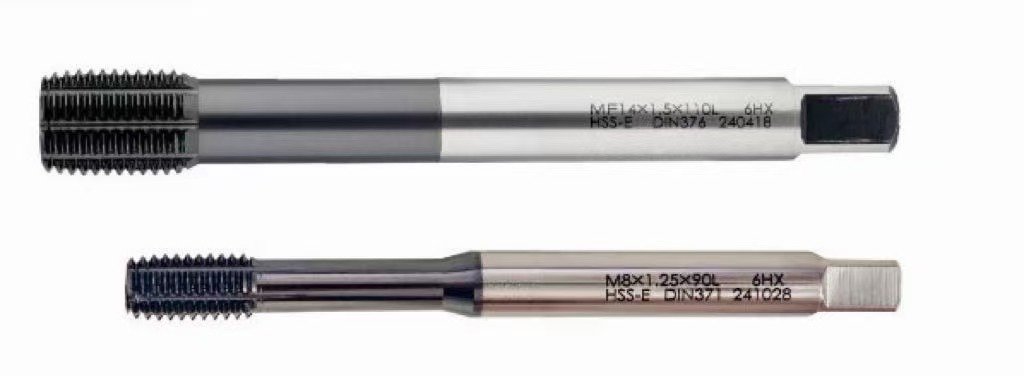
DIN Forming Taps
HSS-E forming taps for chipless internal threading in ductile materials, including steel, stainless steel, copper and aluminium.
M3–M20 · DIN 371 / 376 / 374
Model Specifications
Dimensions are in millimetres. Select the thread diameter, pitch and complete EDP order code.
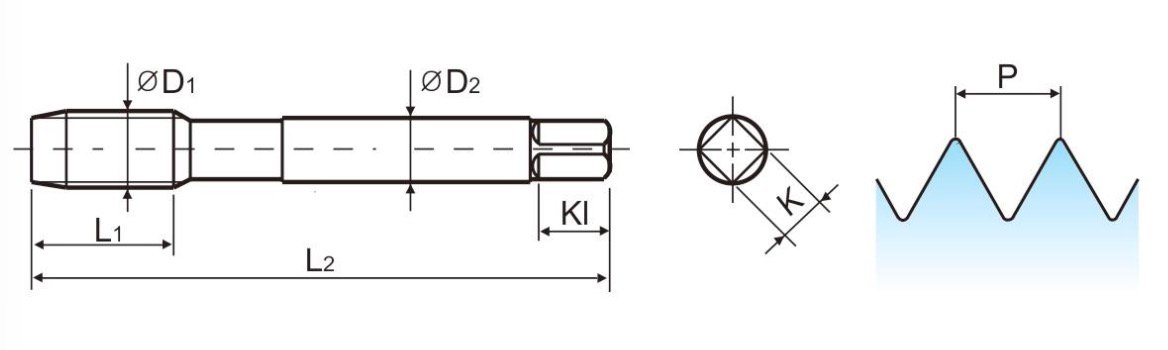
| Thread D1 | Pitch P (mm) | EDP order code | Tolerance | Overall L2 (mm) | Thread + neck L1 (mm) | Shank D2 (mm) | Square K (mm) | Square length Kl (mm) | Grooves |
|---|---|---|---|---|---|---|---|---|---|
| M3 | 0.5 | MG03206 | 6HX | 56 | 18 | 3.5 | 2.7 | 6 | 1 |
| M4 | 0.7 | MG03246 | 6HX | 63 | 21 | 4.5 | 3.4 | 6 | 1 |
| M5 | 0.8 | MG03286 | 6HX | 70 | 25 | 6 | 4.9 | 8 | 2 |
| M6 | 1 | MG03316 | 6HX | 80 | 30 | 6 | 4.9 | 8 | 2 |
| M8 | 1 | MG03376 | 6HX | 90 | 35 | 8 | 6.2 | 9 | 6 |
| M8 | 1.25 | MG03366 | 6HX | 90 | 35 | 8 | 6.2 | 9 | 6 |
| M10 | 1 | MG03446 | 6HX | 100 | 39 | 10 | 8 | 11 | 8 |
| M10 | 1.25 | MG03436 | 6HX | 100 | 39 | 10 | 8 | 11 | 8 |
| M10 | 1.5 | MG03426 | 6HX | 100 | 39 | 10 | 8 | 11 | 8 |
| M12 | 1.25 | MG03526 | 6HX | 110 | 17 | 9 | 7 | 10 | 8 |
| M12 | 1.5 | MG03516 | 6HX | 110 | 17 | 9 | 7 | 10 | 8 |
| M12 | 1.75 | MG03506 | 6HX | 110 | 17 | 9 | 7 | 10 | 8 |
| M14 | 1.5 | MG03556 | 6HX | 110 | 20 | 11 | 9 | 12 | 8 |
| M14 | 2 | MG03546 | 6HX | 110 | 20 | 11 | 9 | 12 | 8 |
| M16 | 1.5 | MG03616 | 6HX | 110 | 20 | 12 | 9 | 12 | 8 |
| M16 | 2 | MG03606 | 6HX | 110 | 20 | 12 | 9 | 12 | 8 |
| M18 | 1.5 | MG03676 | 6HX | 125 | 20 | 14 | 11 | 14 | 8 |
| M18 | 2.5 | MG03656 | 6HX | 125 | 20 | 14 | 11 | 14 | 8 |
| M20 | 1.5 | MG03726 | 6HX | 140 | 20 | 16 | 12 | 15 | 8 |
| M20 | 2 | MG03716 | 6HX | 140 | 20 | 16 | 12 | 15 | 8 |
| M20 | 2.5 | MG03706 | 6HX | 140 | 20 | 16 | 12 | 15 | 8 |
Workpiece Materials
PSteel MStainless Steel NNon-ferrous Metals
Features & Parameters
DIN
Tool standard
371 / 376 / 374
HSS-E
Tool material
Cobalt HSS
6HX
Tap tolerance
Metric thread
2.0P / 4.0P
Chamfer lead
In thread pitches
60°
Thread angle
Metric profile
3.0 × D1
Tapping depth
Blind & through holes
Vap
Surface finish
Bright
Surface finish
TiN
Surface finish
Workpiece Suitability
| Material group | Workpiece material | Condition / grade | Suitability |
|---|---|---|---|
| PSteel | Low-carbon steel | C ≤ 0.25% | Excellent |
| PSteel | Medium-carbon steel | C 0.25–0.45% | Excellent |
| PSteel | High-carbon steel | C ≥ 0.45% | Excellent |
| PSteel | Alloy steel | SCM | Excellent |
| MStainless Steel | Stainless steel | SUS | Excellent |
| NNon-ferrous Metals | Copper | Cu | Excellent |
| NNon-ferrous Metals | Brass | Bs | Excellent |
| NNon-ferrous Metals | Wrought aluminium | AL | Excellent |
| NNon-ferrous Metals | Cast aluminium alloys | AC / ADC | Excellent |
| PSteel | Cast steel | SC | Good |
| NNon-ferrous Metals | Cast zinc alloys | ZDC | Good |
Cutting speeds & coolant
General starting values for forming taps. Adjust to the workpiece, tap finish, hole dimensions and machining conditions.
| Material group | Workpiece | Condition / grade | Speed Vc (m/min) | Neat oil | Water-soluble | Semi-dry | Dry |
|---|---|---|---|---|---|---|---|
| PSteel | Low-carbon steel | C ≤ 0.25% | 8–13 | ◎ | ○ | — | — |
| PSteel | Medium-carbon steel | C 0.25–0.45% | 7–10 | ◎ | ○ | — | — |
| PSteel | High-carbon steel | C ≥ 0.45% | 5–8 | ◎ | ○ | — | — |
| PSteel | Alloy steel | SCM | 5–8 | ◎ | △ | — | — |
| MStainless Steel | Stainless steel | SUS | 5–10 | ◎ | ○ | — | — |
| NNon-ferrous Metals | Copper | Cu | 7–12 | ○ | ○ | — | — |
| NNon-ferrous Metals | Brass / brass castings | Bs / BsC | 7–12 | ○ | ○ | ○ | ○ |
| NNon-ferrous Metals | Wrought aluminium | AL | 7–12 | ◎ | ○ | — | — |
| NNon-ferrous Metals | Cast aluminium alloys | AC / ADC | 12–20 | ◎ | ○ | — | — |
| NNon-ferrous Metals | Cast zinc alloys | ZDC | 7–12 | ◎ | ○ | — | — |
◎, ○ and △ indicate the coolant ratings. A dash indicates no listed recommendation. Cutting speed is in m/min; spindle speed n = 1000 × Vc / (π × D1), with D1 in mm.
| Symbol | Meaning | Unit |
|---|---|---|
| D1 | Nominal thread diameter | mm |
| P | Thread pitch | mm |
| L2 | Overall length | mm |
| L1 | Thread + neck length | mm |
| D2 | Shank diameter | mm |
| K | Square drive width | mm |
| Kl | Square drive length | mm |
| EDP | Complete product order code | — |
DIN 371: metric coarse threads M2–M10. DIN 376: metric coarse threads M11–M30. DIN 374: metric fine threads. Available sizes for this series are listed above.
Forming taps produce threads by displacing material. Pre-hole size must suit the material and forming process; a cutting-tap pre-hole size is not interchangeable.
Confirm pre-hole sizes on the tap drill size chart.
Include the EDP code, surface finish, quantity, workpiece material and hardness, thread depth and coolant method with your enquiry.
EXPLORE THE RANGE